
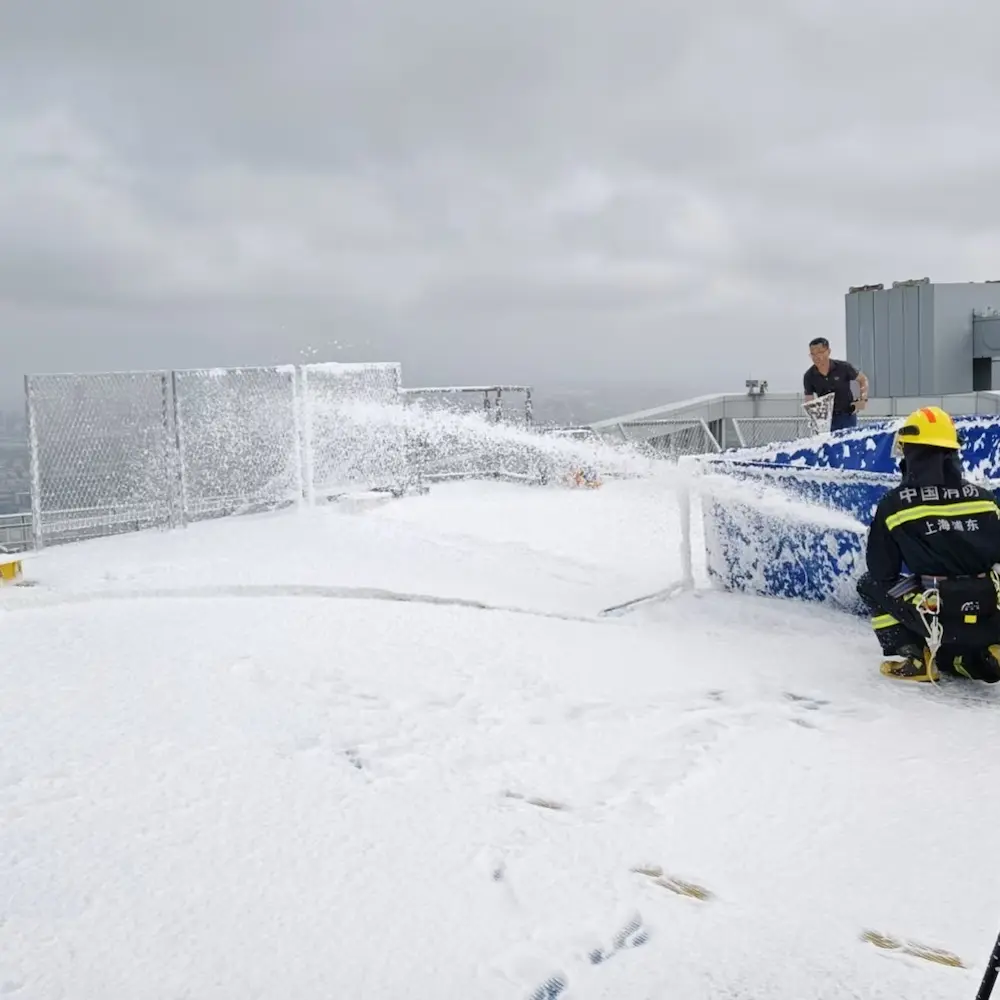
Oil Refineries, Chemical Plants, Ports, and Industrial Sites — Kotech’s Diesel Air Compressor Powers Foam Systems Where It Matters Most
Kotech's diesel-driven compressed air supply module is purpose-built for fire truck foam systems, delivering 6 m³/min (176 CFM) at 20 bar (290 PSI) for foam mixing, discharge, and long-distance delivery. The independent diesel engine allows operation without external power or the host vehicle's main engine, providing flexibility during emergency incidents. Designed for vehicle-mounted integration, the compact module fits standard fire trucks, industrial firefighting vehicles, port response units, and custom rescue platforms. Multiple safety protections—high-temperature shutdown, overpressure protection, low oil pressure alarms, and automatic shutdown—ensure reliable operation under demanding conditions. Easy-access service points simplify maintenance and keep the system mission-ready. The module is deployed across oil depots, chemical plants, port facilities, and industrial firefighting fleets throughout China.
Contact Us NowCustomer Pain Points
Firefighting foam systems are only as effective as the compressed air that drives them. Whether it's a blazing oil depot, a chemical plant with volatile hydrocarbons, or a port facility handling flammable liquids, the ability to generate and deliver high-quality foam quickly is the difference between a contained incident and a catastrophe.
A major Chinese fire truck manufacturer and several industrial end-users had been struggling with a common problem: the compressed air supply for their foam systems was unreliable. The existing solutions—either truck-mounted engine-driven compressors or external air supply connections—had significant limitations:
Dependence on external power. Many industrial sites lacked reliable electrical outlets at the point of use, and truck-mounted systems often drew power from the vehicle's main engine, which meant the foam system couldn't operate independently if the truck was idling or the engine was needed for other functions.
Insufficient pressure and flow. Standard workshop compressors couldn't deliver the 20 bar pressure needed for long-distance foam delivery or the 5 m³/min flow required for sustained foam output. The result was weak foam, poor coverage, and wasted time.
Maintenance headaches. Existing compressors were often built into fire trucks without consideration for service access. Replacing air filters or performing routine maintenance required disassembling half the truck body—a scenario that frustrated maintenance crews and extended downtime.
Limited integration flexibility. Each fire truck or emergency vehicle had unique space constraints, and off-the-shelf compressor packages rarely fit the available footprint. Custom solutions were expensive and slow to deliver.
The fire truck manufacturer's engineering manager put it bluntly: "We need a compressor package that works every time, delivers the pressure and flow we spec, and doesn't require us to redesign the truck around it. Something we can bolt in and trust."
Solutions
Kotech developed a diesel-driven compressed air supply module specifically designed for fire truck foam systems. This standalone package delivers 5 m³/min (176 CFM) at 20 bar (290 PSI) —sufficient flow and pressure for continuous foam output, long-distance hose runs, and demanding industrial firefighting scenarios.
The system is built around a purpose-selected diesel engine, independent of the host vehicle's power plant. This means the foam system can operate even when the truck's main engine is off, providing operational flexibility during complex rescue incidents. The diesel drive also eliminates the need for external electrical connections, making the module suitable for remote or off-grid sites.
Key design features address the client's pain points directly:
Stable 6 m³/min air delivery at 20 bar. The compressor is matched to the engine output to ensure consistent pressure and flow. This supports stable foam mixing, reliable discharge, and long-distance delivery—critical for reaching deep into tank farms or across large industrial sites.
Vehicle-mounted integration. The package is compact and structurally reinforced for vehicle installation. It can be mounted on fire trucks, emergency rescue vehicles, industrial firefighting vehicles, and custom vehicle platforms. The footprint is designed to fit standard truck compartments without requiring major modifications.
Multiple safety protections. The system includes high-temperature shutdown, overpressure protection, low oil pressure alarms, and automatic shutdown in fault conditions. These features protect both the equipment and the personnel operating it in high-stress environments.
Easy maintenance. Key components—air filters, oil filters, and service points—are arranged for quick access. Daily inspections can be performed without removing panels or disassembling other equipment. This design philosophy came directly from Kotech's experience with fire service mechanics who needed to keep equipment operational.
Implementation Steps
- Requirement analysis. Kotech's engineering team worked with the fire truck manufacturer to define the air delivery profile—pressure, flow, duty cycle—and space constraints for the vehicle integration.
- Module configuration. The diesel engine and compressor are matched for the specific performance requirements, with the cooling system, air intake filtration, and exhaust routing configured for the intended installation.
- Safety system integration. The protection systems are calibrated and tested to ensure reliable operation under emergency conditions, including high-temperature and overpressure scenarios.
- Installation and integration. The completed module is installed on the vehicle platform, with connections to the foam proportioning system and discharge equipment. Kotech provides installation supervision and support.
- Commissioning. Each system is run through a full performance test, verifying air delivery, pressure stability, and safety system functionality.
- Training. End-user firefighting crews and maintenance personnel are trained on operation, daily inspection, and preventive maintenance procedures.
Key Parameters
| Multiple safety protections are built into the system | high-temperature shutdown, overpressure protection, low oil pressure alarms, and automatic shutdown in fault conditions. These features protect both the equipment and the personnel operating it in high-stress emergency environments. |
|---|
Customer results
Products Used in This Case

FAQ (Frequently Asked Questions)
Why does a fire truck foam system need a dedicated compressor instead of using the vehicle's engine?
Fire truck foam systems require stable, high-pressure air (20 bar) at consistent flow (6 m³/min) during foam discharge—a demand that's difficult to meet with an engine-driven compressor running off the vehicle's main engine. A dedicated diesel compressor module operates independently, so the foam system works whether the truck engine is running or not. It also provides better flow stability and reduces wear on the vehicle's primary engine.
What applications is this diesel compressor module suitable for?
This package is designed for firefighting and emergency foam systems across multiple platforms, including fire trucks, industrial firefighting vehicles, port emergency response vehicles, and custom rescue platforms. The applications include oil depots, chemical plants, ports, industrial sites, and emergency rescue operations.
What air delivery and pressure does the module provide?
The module delivers 6 m³/min (176 CFM) at 20 bar (290 PSI). This is sufficient for foam mixing, discharge, coverage, and long-distance delivery—including hose runs of up to 150 metres or more, depending on hose diameter and layout.
How is the module protected against failure during operation?
The module includes multiple safety protections: high-temperature shutdown, overpressure protection, low oil pressure alarms, and automatic shutdown in fault conditions. These features protect both the equipment and the personnel operating it during emergency incidents.