
Kotech KOE-110(VSD) Frequency-Controlled Compressor Optimizes Energy Use in Turkey’s Power Generation Industry
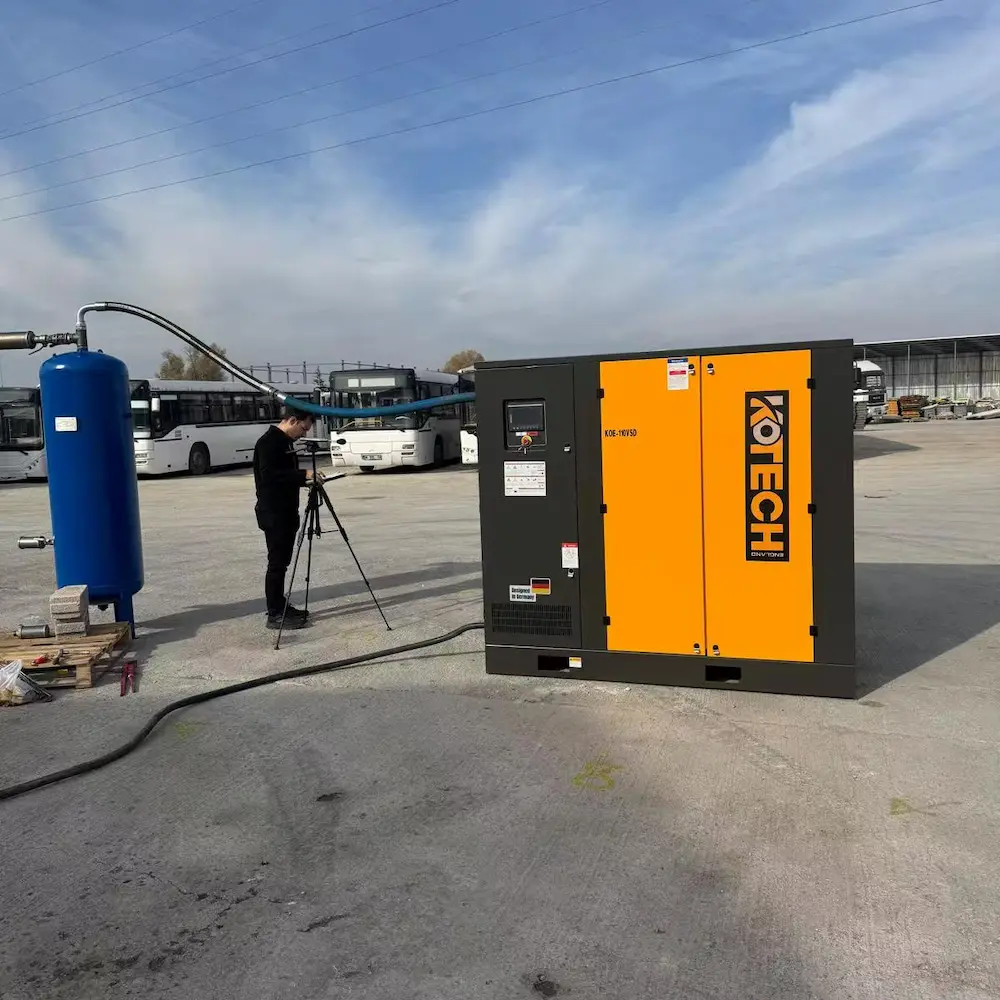
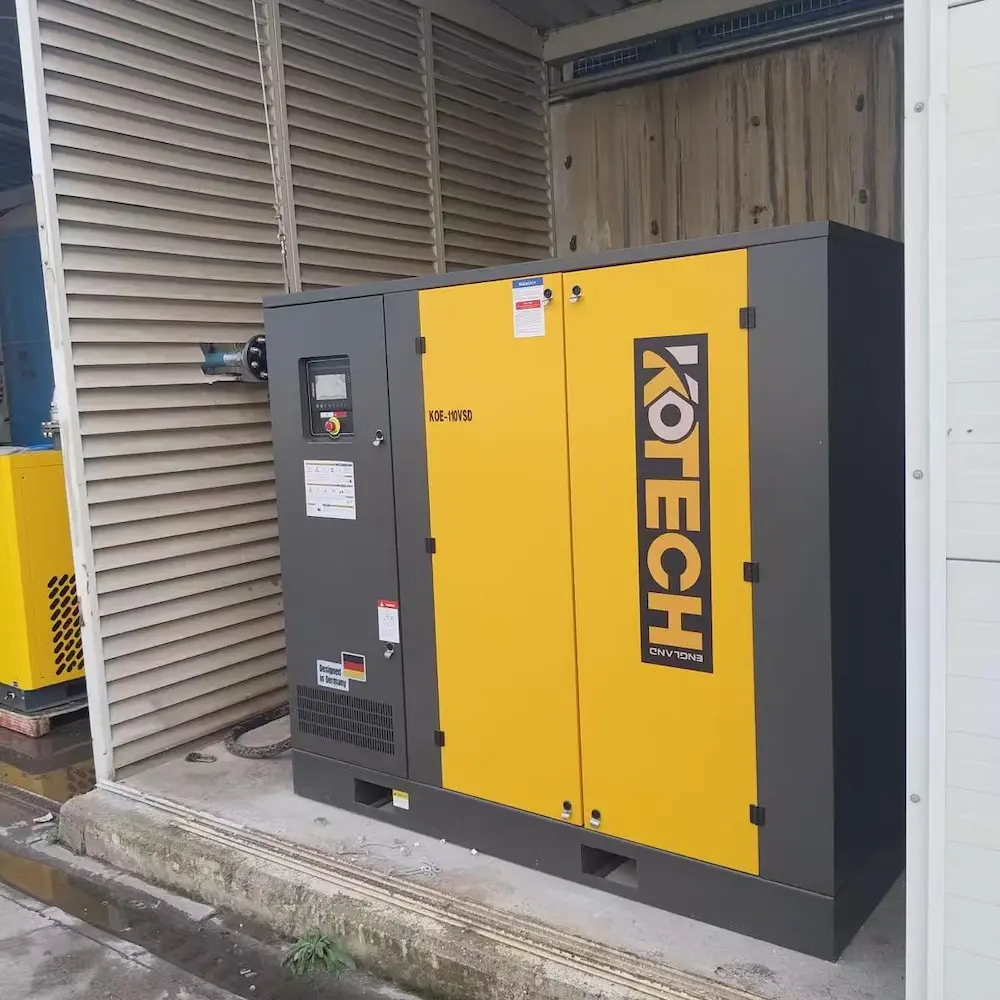
The Kotech KOE-110(VSD) variable speed drive oil-injected screw compressor was deployed at a thermal power plant in Turkey's Muğla province to replace a fleet of fixed-speed compressors supplying instrument air and service air. The VSD technology matches motor speed to real-time demand, eliminating the energy waste of fixed-speed units during partial-load operation. Over the first six months, the compressor achieved 30% energy savings compared to the previous fixed-speed baseline, maintained stable 8.5 bar pressure for pneumatic actuators and control valves, and logged 99.5% uptime with no unscheduled maintenance. The case study demonstrates the KOE-110(VSD)'s effectiveness for 24/7 power generation applications where reliability and energy efficiency are critical.
Get a QuoteCustomer Pain Points
Turkey's power generation sector relies heavily on domestic lignite coal, with plants like the Yeniköy and Kemerköy facilities in the Gökova Bay region generating approximately 5% of the country's electricity . But keeping a thermal power plant running 24/7 isn't just about burning coal—it's about keeping every auxiliary system operational, and compressed air is one of the most critical.
A large thermal power plant in Turkey's Muğla province was running a fleet of fixed-speed air compressors to supply instrument air and service air across the facility. The plant's operations team had been dealing with three persistent problems that were eating into their budget and reliability.
Energy waste was the first issue. The fixed-speed compressors ran at full capacity regardless of demand. At night, when instrument air consumption dropped, the compressors would still run at 100% and then unload—a cycle that wasted a significant amount of electricity . The plant's energy manager had tracked the numbers and knew that compressed air accounted for roughly 12–15% of the facility's auxiliary power consumption. With Turkey's industrial electricity prices climbing, every wasted kilowatt-hour meant real money.
Pressure fluctuations were the second headache. The plant's compressed air system fed pneumatic actuators, control valves, and soot-blowing systems across the boiler house and turbine hall. When the fixed-speed compressors cycled on and off, pressure would spike and dip. The instrumentation team had documented several instances where pressure drops had caused control valves to respond sluggishly, affecting combustion control and emission readings. The operations supervisor put it this way: "The plant runs on instruments. When air pressure gets unstable, the instruments get nervous. And that makes us nervous."
Maintenance costs were climbing. The fixed-speed compressors started and stopped frequently, and every start put wear on the motor and airend. The maintenance team was replacing contactors and servicing airends more often than the manufacturer's schedule suggested. The plant's maintenance manager estimated that they were spending roughly 30% more on compressor maintenance than they had budgeted.
Solutions
Kotech deployed the KOE-110(VSD) variable speed drive oil-injected screw compressor, specifically selected for its ability to match air supply to actual plant demand.
The KOE-110(VSD) is powered by a 110kW high-efficiency motor with an integrated variable frequency drive. Unlike fixed-speed units that run at 100% regardless of demand, the VSD technology adjusts motor speed to match the plant's real-time air consumption . At full capacity, the unit delivers up to 20 m³/min at 8.5 bar—enough to cover peak demand during soot-blowing cycles and high-load periods. During off-peak hours, the compressor ramps down to partial load, saving energy without compromising system pressure .
The variable speed drive also eliminates the pressure spikes and dips that had been troubling the plant's instrumentation. By continuously adjusting compressor output, the KOE-110(VSD) maintains a stable system pressure within a narrow band. This means pneumatic actuators and control valves see consistent air pressure, improving process stability.
The KOE series is built with a robust oil-injected screw airend, capable of operating in ambient temperatures up to 46°C and handling the dusty environment of a coal-fired power plant . The unit also features a modern touchscreen controller that integrates with the plant's control system, allowing remote monitoring and real-time performance tracking.
Implementation Steps
- Plant air demand assessment. Kotech engineers analysed the plant's compressed air usage profile across a full 24-hour cycle, identifying peak demand periods (soot-blowing, startup) and low-demand periods (night shifts).
- VSD compressor configuration. The KOE-110(VSD) was configured with the plant's pressure setpoints and programmed for energy-optimized operation.
- Equipment delivery and installation. The unit was delivered to the power plant and installed in the existing compressor room, with minimal disruption to ongoing operations.
- Integration with plant control system. The compressor's controller was integrated with the plant's DCS, allowing operators to monitor performance and receive maintenance alerts.
- Commissioning and performance verification. The unit was run through a full operating cycle, with technicians verifying pressure stability, energy consumption, and motor performance.
- Operator training. Plant staff were trained on VSD operation, setpoint adjustment, and routine maintenance procedures.
Customer results
Products Used in This Case

FAQ (Frequently Asked Questions)
Why is variable speed drive (VSD) technology better for power plant applications?
Power plants have variable compressed air demand. During peak operation, instrument air and soot-blowing systems require high flow; during night shifts or low-load periods, demand drops significantly. Fixed-speed compressors run at full capacity regardless of demand, wasting energy during unload cycles. VSD compressors adjust motor speed to match real-time demand, saving up to 35% energy in typical power plant installations
What's the difference between the KOE-110 fixed-speed and the KOE-110VSD?
The fixed-speed model runs at a constant motor speed, cycling on and off to maintain system pressure. The VSD model uses a variable frequency drive to continuously adjust motor speed, maintaining stable pressure with minimal pressure fluctuation and lower energy consumption during partial-load operation
How does the KOE-110(VSD) maintain stable instrument air pressure?
The VSD system continuously monitors system pressure and adjusts motor speed in real time. When demand increases, the compressor ramps up; when demand drops, it ramps down. This eliminates the pressure spikes and dips caused by fixed-speed compressors cycling on and off, ensuring stable air supply for pneumatic actuators and control valves.
What kind of energy savings can a thermal power plant expect with the KOE-110(VSD)?
In the Turkish power plant project, the KOE-110(VSD) reduced compressed air system energy consumption by approximately 30–35% compared to fixed-speed units operating under the same demand profile. Savings are highest during partial-load periods, which make up a significant portion of a power plant's operating hours